
Sensors, IoT & Telemetry · Engineering example
Modernizing Existing Equipment Without Replacing It
Keep a mechanically useful machine in service while adding carefully chosen measurements, a trustworthy event history, and a protected read-only path to business reporting. Modernization starts with the decision the operation needs, not with a blanket controller replacement.
The operating challenge
An older machine can still be the right machine.
A press, mill, mixer, or packaging line may deliver acceptable product for years after its controller and data interfaces become dated. Replacing it solely to gain a dashboard can introduce capital cost, qualification effort, downtime, and a new training burden. Yet running it without reliable production and condition history leaves teams guessing about short stops, setup losses, recurring faults, and maintenance needs.
Useful assets, limited visibility
Operators know what the machine is doing, but the evidence lives in shift notes, panel counters, and local alarms rather than a shared timeline.
Connectivity can add risk
An unsupported controller may not tolerate modern network traffic or direct internet access. Monitoring must not compromise its timing or control functions.
Signals need meaning
A current draw or cycle pulse does not alone mean good production. Job, material, inspection, and operator reason codes explain what the signal represents.
Why modernize: Preserve the equipment investment while making loss, quality, and maintenance questions answerable. The goal is an evidence-bearing operational layer, not an automatic claim that every old machine should be connected.
Illustrative operating example
A reliable hydraulic press has no useful event history.
This hydraulic-press situation is illustrative. It is not a claim about a completed customer installation, measured savings, or an engineering approval for a specific retrofit.
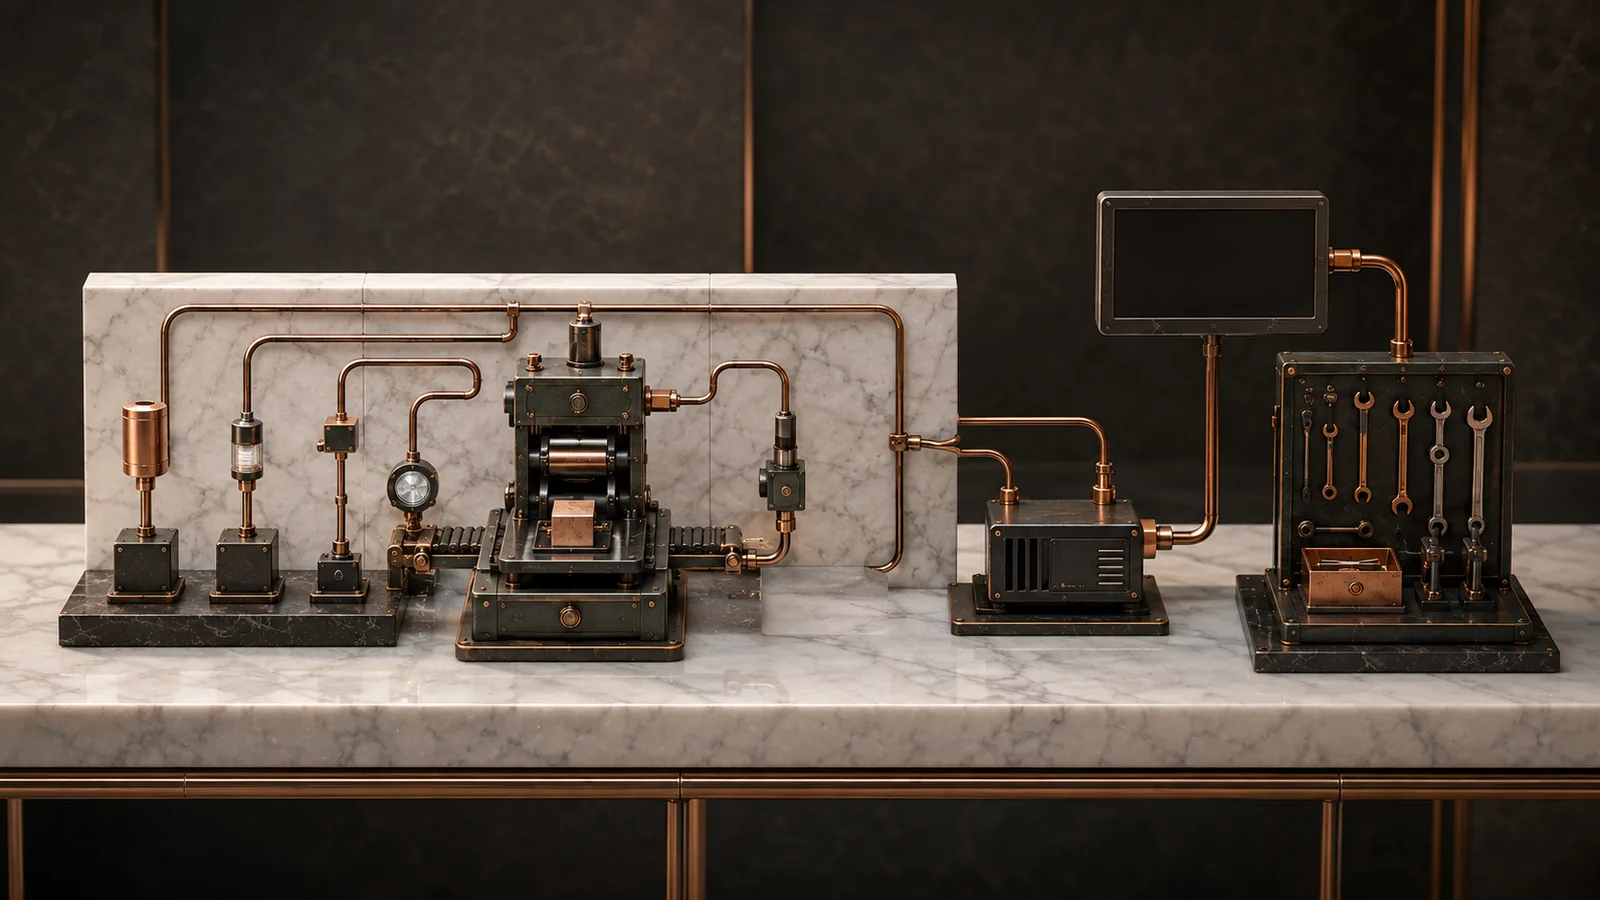
Imagine a hydraulic press that makes a critical formed component. Its mechanical structure is sound, but the panel provides only a total cycle count and a short fault list. Supervisors see that accepted output varies between shifts. Operators report occasional pressure recovery delays and material waits, while maintenance suspects valve wear. A new controller would be a major project. A bounded first step is to instrument what can be measured without changing the press control circuit, then reconcile those observations with job, quality, and operator records.
- Inspect the machine and boundaries.Maintenance, controls engineering, and safety personnel review drawings, power, guarding, available signals, installation locations, and what must remain untouched.
- Choose a narrow question.Start with cycle timing and accepted output by job, or pressure recovery under comparable load. Avoid collecting signals without a decision they can support.
- Add nonintrusive observation.Where approved, use isolated read-only outputs or external sensors and an edge collector. Record calibration, time source, and sensor health.
- Join operating context.Bring in scheduled job, material lot, inspection result, maintenance event, and concise operator reason for a pause. Preserve missing context as unknown.
- Test an intervention.The team may inspect the hydraulic system, stage material differently, or adjust a maintenance interval. Compare similar jobs before claiming improvement.
What the reviewer would see
Press H-7: a trustworthy first timeline
Observable facts are separated from possible causes and authorized decisions.
- Machine context
- Asset H-7, job, shift, material, and effective setup.
- Observed evidence
- Cycle edges, duration, pressure trend, data gaps, and sensor health.
- Production evidence
- Accepted and rejected units with quality-record source.
- Decision
- Maintenance or operations reviews a repeat pattern before changing work or equipment.
Other high-priority situations
The right retrofit depends on the question.
Packaging line loses short intervals
External cycle and motor-state signals can help distinguish running, starved, blocked, and stopped periods when the original control system has no event export. Operators still verify the reason for each meaningful loss.
Useful report: state duration, line context, reason, and accepted packs.
Older pump has no condition trend
Approved temperature, vibration, and motor-current observations can establish a baseline. A technician tests whether changes reflect duty, sensor placement, or an actual maintenance concern.
Useful report: comparable-load trend, inspection finding, and sensor quality.
What a modernization would connect
Make the new data layer independent of machine control.
The design should respect electrical and mechanical boundaries. A retrofit sensor is not free of installation risk; power, isolation, mounting, calibration, network placement, and maintenance access all need review. The edge device should be replaceable without stopping the original machine function.
Required operating evidence
- Asset inventory, drawings, controller limits, and approved connection points
- Machine states, cycle events, pressure or current as justified by the use case
- Sensor accuracy, installation position, calibration, and timestamp quality
- Job, product, schedule, material, inspection, and maintenance context
- Operator-confirmed reasons for setup, waiting, planned stops, and faults
- Data-loss, battery or power, and gateway-health events
A sensor reading becomes useful only when its physical meaning and limitations are documented.
Connected technical layers
- Approved nonintrusive sensors or isolated read-only interfaces
- Local edge collection with buffering and health monitoring
- Segmented, outbound-only or otherwise protected data path
- Historian or event store plus controlled job and quality joins
- Human review and versioned reporting definitions
Control commands, safety circuits, and machine interlocks stay in the original validated system.
A read-only intention should be verified in the electrical design, credentials, protocol permissions, and network test. A dashboard label alone does not make a connection safe.
Where automation and AI fit
Automate the record before predicting the future.
Deterministic automation
Timestamp events, classify only states that have validated definitions, detect gaps, and reconcile cycle signals with accepted output. Preserve raw readings and derived calculations separately.
Condition analytics
Compare similar jobs and operating loads to find changing cycle time or pressure recovery. Establish normal variation and technician-verified examples before adding anomaly models.
Evidence-linked AI assistance
An approved assistant may summarize a recurring pattern with its source intervals, missing data, and candidate checks. It should not call a signal a mechanical failure without qualified investigation.
Human operating authority
Controls engineering approves installation. Operators validate states. Maintenance diagnoses and services equipment. Quality determines whether output is acceptable.
How we examine a proposed solution
AI advisors test whether the retrofit is worth doing.
These Adaptiv Stratum AI advisory roles can support bounded research and design review. They do not certify an electrical installation or control the press.
Argus
Reviews signal identity, timestamp lineage, and data continuity.
Hephaestus
Challenges sensor placement and the physical meaning of press states.
Pythia
Tests whether a trend model adds value over transparent rules.
Aegis
Looks for unsafe connectivity, stale data, and misleading state labels.
Clio
Defines comparable-job evidence for an improvement trial.
Themis
Reviews installation authority, decision rights, and change records.
What becomes visible
Show the old machine's work in operational context.
A good report distinguishes a measured event from an inferred state and a human-verified reason. It also tracks the retrofit itself: a failed sensor must not silently turn into a healthy-looking machine.
Machine and shift view
- Scheduled time, job, product, and effective setup
- Observed cycles, pauses, and unclassified intervals
- Accepted units, rejects, and reconciliation gaps
- Pressure or current trend under comparable operating state
- Operator notes and maintenance events with timestamps
Retrofit and improvement view
- Sensor freshness, missing data, calibration, and gateway uptime
- State-definition versions and manual corrections
- Repeat event frequency and verified cause
- Downtime and first-good-part time by similar job
- Maintenance interventions and after-work trend
- Installation and lifecycle cost versus demonstrated decision value
Higher data volume is not a benefit by itself. Keep only measurements that support a decision and are reliable enough to compare over time.
Operating safeguards
Preserve the useful machine and its safety case.
- Formal engineering review of sensors, power, isolation, and mounting
- Documented read-only boundary with no controller or safety-circuit writes
- Network segmentation and limited, monitored data flows
- Local buffering and visible gateway or sensor failure
- Calibration and timestamp checks before analysis
- Operator validation of ambiguous machine states
- Accepted output reconciled against quality records
- Rollback removes the monitoring layer without disabling the machine
A practical first phase
Start with one machine and one recurring loss.
- Choose the decision.Agree whether the first question is short stops, pressure recovery, or maintenance timing and how a better answer would change work.
- Inspect existing evidence.Walk the process with operators, review drawings and maintenance records, and identify safe measurement points.
- Install a bounded observer.Engineering approves nonintrusive sensing, segmentation, timestamping, and a no-write architecture.
- Verify the timeline.Compare new readings against physical observation, manual counts, and quality records across representative jobs.
- Test and decide.Trial one maintenance or scheduling improvement. Expand only if the data changes decisions and the retrofit remains reliable and safe.
Begin with a useful asset
What does the machine do well, and what can you not yet see?
The best first retrofit may be a small, carefully governed measurement layer.
Evidence and further reading
Retrofit for a defined decision and protected connection.
These primary sources inform the approach. The hydraulic-press scenario is illustrative, not an Adaptiv Stratum customer case study.
- NIST: Supporting Digital Transformation with Legacy Components discusses legacy connectivity limits and OT security considerations.
- NIST and ASME: When and Where PHM Should Be Integrated frames asset selection around safety, operational value, baseline, and cost-effective condition management.
- NIST: Industry 4.0 and Cybersecurity explains why equipment-monitoring investments need OT security review.