
Predictive Maintenance
Predictive Maintenance vs. Preventive Maintenance
Choose maintenance logic according to failure behavior, evidence, intervention opportunity, and consequence, not terminology.
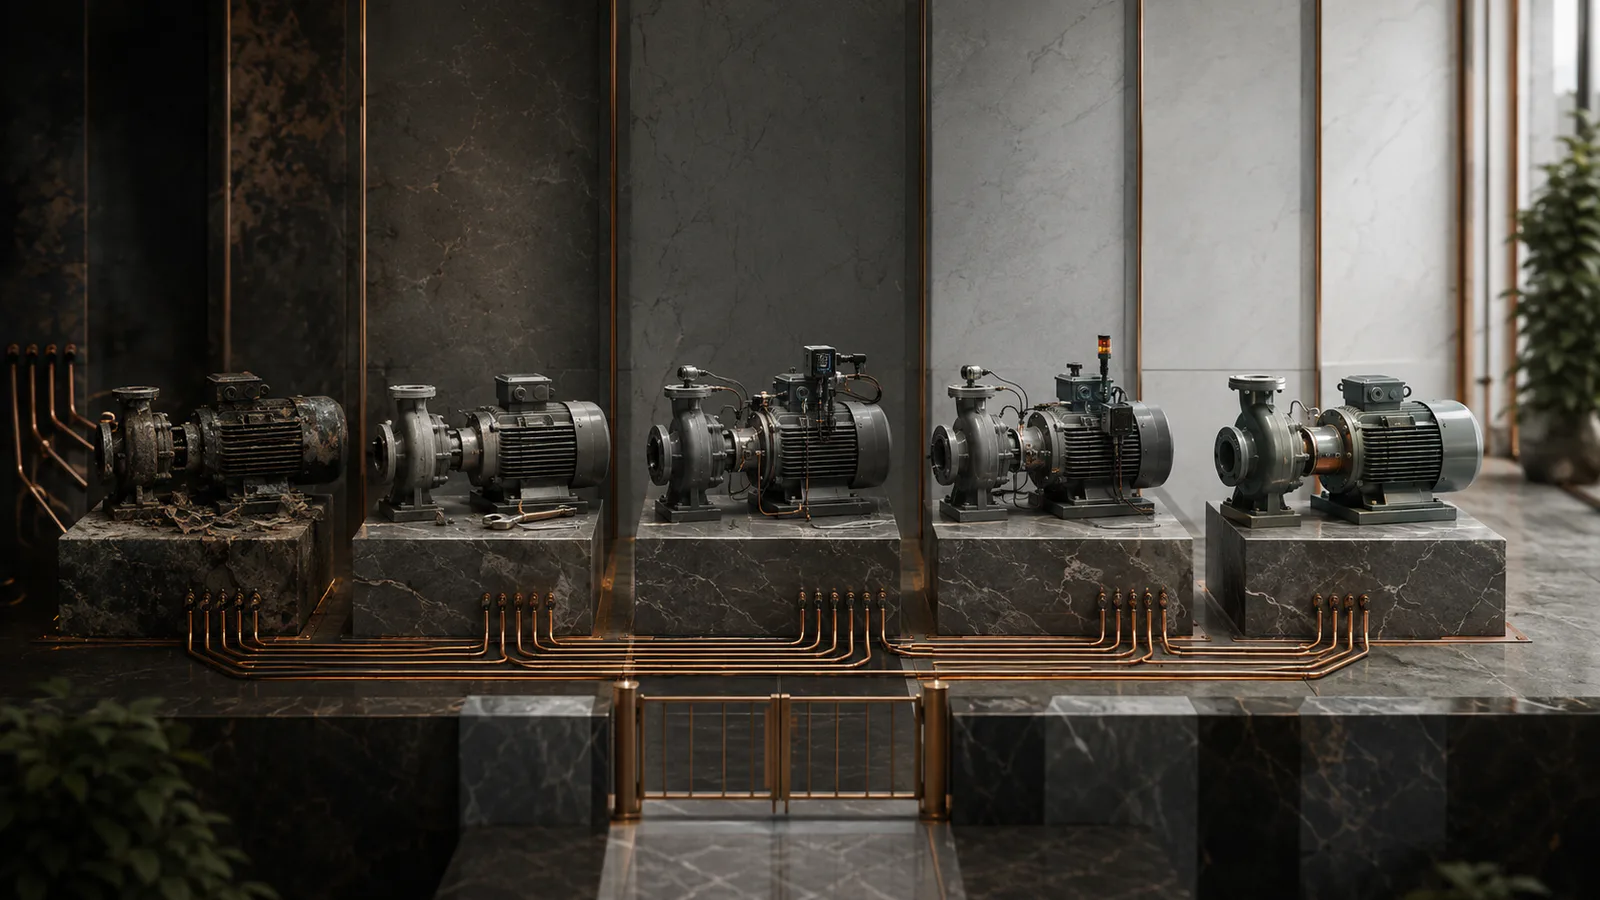
Preventive maintenance acts on a schedule, usage interval, or established service rule. Predictive maintenance attempts to estimate a future condition from measured evidence. Condition-based maintenance acts when a defined present condition is observed.
These approaches can coexist. The objective is not to label the program predictive; it is to reduce failure and maintenance cost without creating unsafe delay or false confidence.
Engineering consideration
When preventive maintenance is strong
Scheduled work is appropriate when age or usage is a credible risk driver, inspection intervals are established, measurement is impractical, or the consequence requires conservative intervention. A predictable task may not benefit from a model.
Engineering consideration
What prediction requires
A predictive approach needs stable asset identity, relevant sensors, operating context, known maintenance events, observable deterioration, enough lead time for useful action, and evidence that the signal relates to the failure mode.
- Defined failure mode
- Reliable condition history
- Known interventions and outcomes
- Actionable warning horizon
- Measured false alarms and missed events
Engineering consideration
Evaluate the combined program
Compare cost, downtime, risk, inspection burden, parts planning, and verified outcomes. A condition signal may adjust one preventive interval while safety-critical tasks remain fixed.
Questions worth answering
Before selecting the technology
- Which failure mode are we trying to manage?
- Is deterioration observable before failure?
- Would earlier information change a maintenance decision?
- What happens when the prediction is wrong?
The engineering decision
Use preventive, condition-based, and predictive methods where each is justified, and evaluate the maintenance outcome rather than the sophistication of the label.
The correct decision depends on the operating requirement, failure consequence, available evidence, and ability to act on the result. Technology should be selected after those constraints are understood.