
Industrial Automation · Engineering example
Industrial Vision Inspection
Make inspection repeatable without turning a camera score into an unexplained quality decision. Define the defect, control image capture, link each result to the unit and recipe, and route uncertain findings to an authorized reviewer.
The operating challenge
Inspection at line speed is only useful if the finding can be trusted.
A visual check may protect assembly quality, labeling, traceability, or a critical feature. Yet manual inspection can vary with fatigue and difficult viewing conditions, while an unvalidated camera system can reject good product or miss defects under a different light, part position, or product revision. The goal is a repeatable measurement and a clear disposition path, not a high model score on a curated image set.
The defect must be defined
“Looks wrong” is not an acceptance criterion. Quality staff need the feature, tolerance or visual standard, product variant, and what must happen when an image cannot be interpreted.
Image conditions change
Lighting, lens focus, fixturing, contamination, motion, and replacement parts can alter an image even if product quality has not changed.
False decisions have cost
A missed defect can escape to a customer; a false reject can create scrap or unnecessary rework. Validation must examine both, with extra attention to rare but consequential failures.
Why modernize: Give quality teams earlier, consistent evidence and a traceable path from detection to disposition and corrective action. Automation earns authority only after the measurement system and response process are proven for the specific product.
Illustrative operating example
A connector assembly needs a visible pin and readable label.
This inspection cell is illustrative. It is not a claim about a completed customer installation, certified inspection accuracy, or a guaranteed reduction in defects.
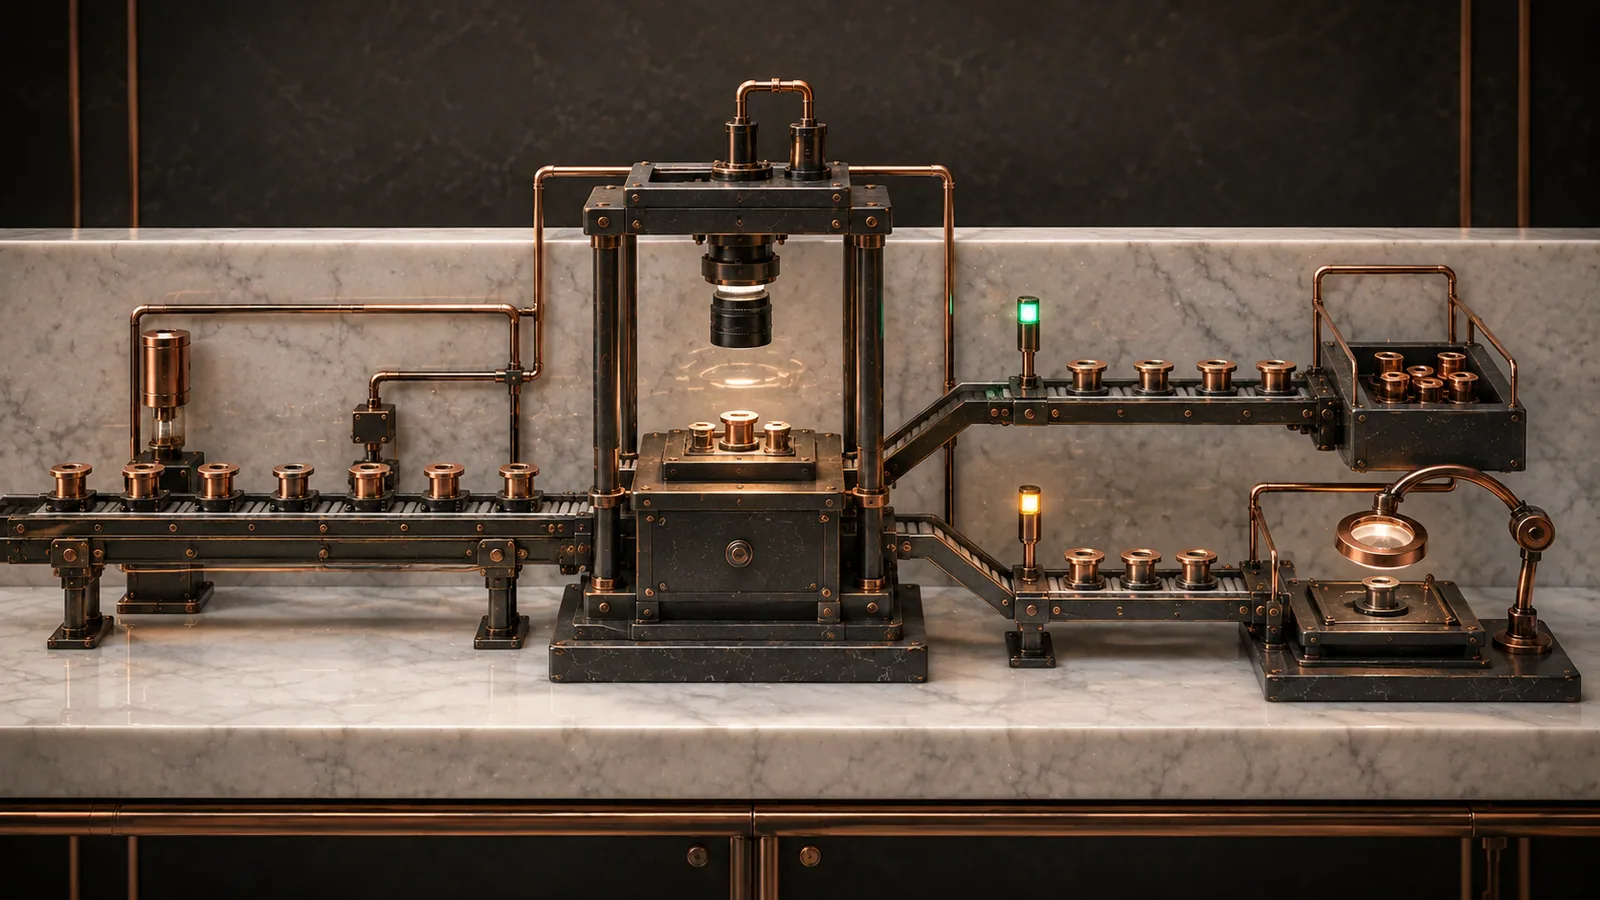
Imagine a station where a connector assembly is placed in a fixture before packaging. An overhead camera checks that a specified pin is present and correctly seated, and that the label code matches the work order. During one shift, the system starts flagging more “missing pin” images. The parts may be defective, but a loose fixture or changed light angle can also hide the pin. The team must not automatically scrap the lot or release it because an AI model is confident.
- Establish the standard.Quality engineering defines the accepted pin position, label content, product variants, and escalation for unreadable images. Approved reference parts include real borderline and known-defective examples.
- Control acquisition.Confirm camera and lens identity, lighting, exposure, trigger, fixture position, part orientation, and image-quality checks before interpreting a frame.
- Separate the checks.A geometric or feature rule may verify the pin, while code reading compares the label to the current work order. Each check records its own evidence and uncertainty.
- Route exceptions.If the feature is absent, the code mismatches, or the image is not trustworthy, the product follows the approved hold/review path. A quality reviewer determines disposition and whether adjacent units need containment.
- Investigate the trend.Compare findings by camera setup, fixture, batch, and shift. If a loose fixture caused false rejects, repair it and retest the inspection method against the approved standard.
What quality would see
Connector Cell 3: pin review required
The image and result are tied to the unit. A review flag is not a final reject or release decision.
- Unit and context
- Serial or lot, product revision, work order, station, time, and camera/recipe version.
- Finding
- Pin region below the approved rule or model confidence boundary; label check reported separately.
- Image quality
- Focus, lighting, orientation, and fixture checks shown with the original frame.
- Disposition
- Authorized quality reviewer records accepted, reworked, scrapped, or held, with reason and scope.
Other high-priority situations
Use the method where evidence can change the decision.
Labels and traceability marks
Verify code presence, readability, and agreement with the order or batch. A readable code that belongs to the wrong product is still a quality problem. Keep the captured image and decoded value linked to the unit.
Useful report: code value, expected value, image quality, mismatch reason, and disposition.
Surface or weld appearance
Appearance can vary legitimately with finish, angle, and product revision. Begin with quality-approved examples and a clear defect taxonomy. A learned model may assist review, but its detection limits and uncertain cases need independent validation.
Useful report: defect class, location, confidence boundary, reference standard, and adjudicated result.
What a modernization would connect
Keep the image, rule, unit, and disposition together.
The technical design starts with repeatable acquisition and reliable unit identity. It then ties a versioned inspection recipe to the correct product and records the actual quality decision. A local safety and reject mechanism, where approved, remains governed by the existing equipment and quality process.
Required operating evidence
- Unit or lot ID, order, product revision, and inspection recipe
- Camera, lens, lighting, fixture, trigger, and calibration version
- Original image and image-quality status with retention rules
- Feature result, defect type, location, and threshold or model version
- Quality review, reinspection, hold, rework, and final disposition
- Line state and relevant maintenance or setup changes
Unusable or unmatched images remain unknown; they do not become automatic passes.
Connected technical layers
- Controlled vision cell and existing local equipment interlocks
- MES or order lookup for the current unit and product recipe
- Versioned rules or evaluated model with an evidence store
- Quality management workflow for containment and disposition
A camera outage must lead to the approved alternate inspection or hold process, not a silent bypass.
A training label is not automatically ground truth. Before deployment, quality engineers must agree on adjudication, sampling, and how to handle ambiguous or rare defects.
Where automation and AI fit
Use the simplest valid method for each check.
Deterministic checks
Read a code, verify presence or geometry under controlled lighting, check image quality, and match the correct recipe to the unit. These steps can already reduce manual transcription and make exceptions easier to investigate.
Learned vision models
For variable appearances that simple rules cannot capture, a model may classify or localize potential defects. Test on held-out production conditions, product revisions, shifts, and rare defects. Revalidate after changes to camera, lighting, fixture, product, or model.
Evidence-linked AI assistance
An approved assistant can summarize clusters of false rejects or compare image findings with setup and maintenance records. It should show image references and contradicting evidence; it cannot declare final product acceptance.
Human quality authority
Qualified quality staff define standards, adjudicate uncertain cases, approve containment and release, and decide when automated disposition is permissible. Operational safety and approved inspection fallback remain independent.
How we examine a proposed solution
AI advisors help challenge the inspection design.
These Adaptiv Stratum AI advisory roles support bounded research and review. They are not human inspectors or a claim that named agents make production release decisions.
Argus
Reviews image capture, station identity, lighting change, and data lineage.
Pythia
Challenges model selection, validation splits, and error by defect class.
Hephaestus
Checks camera-cell integration and local equipment boundaries.
Aegis
Examines missed-defect and false-reject failure modes and fallback.
Clio
Reviews independent reference labels and before-and-after evidence.
Themis
Checks disposition authority, traceability, and claims about accuracy.
What becomes visible
Measure both defect detection and the cost of being wrong.
A unit record supports immediate disposition; a quality-program view shows whether the inspection method is dependable across product variants and time. Review counts without an independent reference are not an accuracy measure.
Per-unit evidence
- Unit, lot, product revision, work order, and station
- Original image, acquisition quality, camera and recipe version
- Each feature or defect finding and its rule or model version
- Hold/review state, reviewer, and final disposition
- Reinspection, rework, and linked corrective action
Program-level measures
- Detection and miss rate by defect type against adjudicated samples
- False rejects, review burden, and reinspection rate
- Image-quality failures and camera or fixture downtime
- Agreement across shifts, products, revisions, and lighting conditions
- Escaped defects and containment events where known
- Time from finding to documented quality disposition
A single aggregate accuracy percentage can hide poor performance on the defect that matters most. Acceptance criteria and validation sampling must reflect the product's actual risk and quality requirements.
Operating safeguards
Fail into a known quality path.
- Quality-approved defect taxonomy, reference parts, and disposition rules
- Image-quality and unit-identity checks before interpretation
- Versioned camera setup, recipe, model, and acceptance criteria
- Test missed defects and false rejects separately, including rare cases
- Retain traceable evidence under an approved retention policy
- Defined hold or alternate inspection when camera or model is unavailable
- Revalidate after product, lighting, fixture, or software changes
- Keep human quality release and containment authority explicit
A practical first phase
Start with one visible feature and a quality-owned standard.
- Pick a decision.Choose a defect or label check where earlier, more consistent evidence would change containment or rework.
- Define reference truth.Have quality staff agree on pass, fail, and ambiguous examples, including product variants and realistic borderline cases.
- Stabilize acquisition.Set the fixture, lighting, trigger, identification, and image-quality requirements before choosing an algorithm.
- Run in parallel.Compare read-only findings with the current approved inspection and adjudicate disagreements. Track both misses and false rejects.
- Decide on authority.Only after repeatable validation, documented failure response, and quality approval should any automated disposition or line integration be considered.
Begin with a quality question
Which feature is hardest to inspect consistently?
One product revision, an approved reference standard, and a small set of real production images can frame the first review.
Evidence and further reading
Validate the measurement, not only the model.
These primary NIST resources inform the method. The connector scenario is illustrative, not an Adaptiv Stratum customer case study.
- NIST: AI-enhanced manufacturing monitoring testbed describes inspection points and high-fidelity process data used to evaluate methods.
- NIST: Detection and segmentation of manufacturing defects illustrates a learned method for difficult defect images, not a general proof of suitability for every line.
- NIST: Performance evaluation for manufacturing perception discusses calibration and benchmarking against controlled ground truth.